6 Best Vacuum Pump Oils For Industrial Systems Pros Use
Maximize the performance of your machinery with these 6 best vacuum pump oils for industrial systems. Read our expert guide to choose the right lubricant today.
Vacuum pump oil is the lifeblood of any HVAC/R evacuation process, often taken for granted until a system fails to pull down to a proper micron level. High-quality oil doesn’t just lubricate; it seals internal clearances and traps moisture, contaminants, and acid that would otherwise ruin a pump’s rotary vanes. Using the wrong weight or a low-grade lubricant is a recipe for premature equipment failure and wasted hours on a job site. Selecting the right fluid ensures that vacuum pumps maintain peak efficiency, whether pulling a vacuum on a large commercial chiller or a standard residential split system.
Disclosure: As an Amazon Associate, this site earns from qualifying purchases. Thank you!
JB Black Gold: The Trusted Workhorse Oil


JB Black Gold is a staple in many tool bags because it handles high-heat environments with consistent stability. When the ambient temperature on a flat roof pushes the limits of a pump, this oil resists breaking down under thermal stress.
This lubricant is specifically engineered to be moisture-tolerant, which is critical when dealing with systems that have sat open to the humid air. Its high viscosity index keeps the pump running smoothly during extended evacuation cycles.
Bottom line: Choose this oil when reliable performance in varying climate conditions is the priority. It is a predictable choice that rarely disappoints on long, grueling industrial jobs.
Robinair Premium: Best for Everyday Reliability

Robinair Premium is widely recognized for its high-vacuum performance across a broad range of pump brands. It remains thin enough to ensure quick startup times even in cooler temperatures, preventing the strain that thicker oils can put on a motor.
This oil is formulated to minimize carbon buildup, which is the primary enemy of vacuum pump longevity. Less sludge means the pump vanes stay free, maintaining the tight tolerances required for deep vacuums.
Bottom line: This is a solid, go-to lubricant for daily service calls. It balances cost and quality, making it an excellent choice for a well-stocked service truck.
Yellow Jacket SuperEvac: Top Choice for HVAC/R
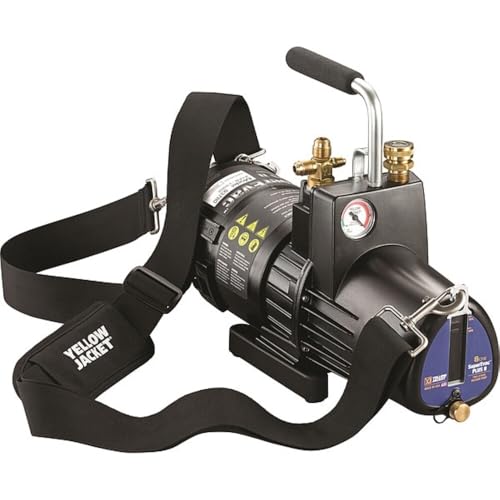
Yellow Jacket SuperEvac is designed for those who demand maximum pump efficiency during deep vacuums. It features a high-density formula that helps create a superior seal between the vanes and the stator, effectively reducing internal leakage.
It is particularly effective at cold-weather start-ups where standard oils might become sluggish. For contractors working in early spring or late autumn on metal roofs, this oil ensures the equipment doesn’t bog down during the initial pull.
Bottom line: If the primary goal is reaching and maintaining low micron levels quickly, SuperEvac is a professional-grade solution. It justifies the price through speed and consistent vacuum stability.
ULVAC R-7: Premium Pick for Deep Vacuum Levels
ULVAC R-7 is a high-purity oil designed for precision applications where every micron counts. This is not for the everyday refrigerant flush, but for critical infrastructure or sensitive industrial systems where contamination must be zero.
The chemical stability of this oil prevents the chemical reactions that occur when oil meets residual refrigerants or acids. It creates an incredibly thin, stable film that allows pumps to achieve their absolute lowest rated vacuum limits.
Bottom line: Use this oil for specialized, deep-vacuum work. While it comes at a premium, the protection it offers for high-end, expensive pumps is unmatched.
NAVAC NPO1: Great Value for High-Performance

NAVAC NPO1 represents a modern approach to vacuum oil, optimized for the high-speed pumps frequently seen on job sites today. It offers excellent moisture separation, which is vital when a system’s filter-drier has been compromised.
The oil’s synthetic blend provides a stable operating temperature, preventing the pump from overheating during long evacuation runs. It is designed to be highly versatile, performing well across a wide spectrum of humidity and ambient heat.
Bottom line: For those seeking a high-performance oil without the extreme price tag of specialty lubricants, this is a top-tier contender. It provides excellent value for high-volume service work.
Accu-Tools BluVac: Engineered for System Purity
Accu-Tools BluVac oil is engineered with a focus on high-purity standards that prevent the outgassing often seen in lower-grade lubricants. Outgassing can artificially inflate micron readings, leading to false indicators that a system is ready for charging.
This oil is designed to work in synergy with advanced digital micron gauges, ensuring the readings on the screen are an accurate reflection of the system’s condition. It is a precision tool component rather than just a lubricant.
Bottom line: Serious technicians who prioritize measurement accuracy should reach for this. It eliminates the variables caused by inferior oils, ensuring a more honest evacuation process.
Oil Viscosity & Type: What Your Pump Requires
The golden rule of vacuum pump maintenance is strictly following the manufacturer’s viscosity recommendations. Using an oil that is too thick creates excessive drag, while oil that is too thin will fail to seal the internal vanes properly.
Most industrial pumps require an ISO 46 or ISO 68 grade oil. Always check the manual before pouring; mixing weights can cause the pump to run hot, leading to mechanical wear that is expensive to repair.
Bottom line: Never guess on viscosity. If the manufacturer specifies a certain weight, stick to it to maintain warranty status and optimal pump life.
How Often Should You Change Your Vacuum Pump Oil?
Vacuum pump oil should be changed immediately after every single use, regardless of how short the cycle was. Oil is a sponge; as soon as it interacts with the atmosphere or refrigerant, it begins to lose its ability to seal and protect.
Waiting for the oil to turn dark or milky is a common mistake that leads to internal rust and pitting. A pump running on dirty oil will eventually fail to pull a vacuum below 500 microns, regardless of how good the pump is.
Bottom line: Think of oil changes as an essential part of the job cost, not an optional maintenance step. Fresh oil is the cheapest insurance for an expensive pump.
Spotting Contamination: When Your Oil is Cooked
If the oil appears cloudy or milky, it has absorbed moisture from the system. If it has turned dark or smells like acrid chemicals, it has likely been contaminated by high concentrations of refrigerant or system acid.
Never attempt to “filter” or reuse used oil. Once it has been through the pump, the chemical properties are permanently compromised and it will only serve to degrade the pump’s internal components during the next session.
Bottom line: When in doubt, pour it out. Investing a few dollars in a fresh bottle of oil is significantly cheaper than replacing a seized vacuum pump motor or stator assembly.
Safe and Proper Disposal of Used Pump Oil
Used vacuum pump oil is classified as hazardous waste and should never be poured down a drain or into the soil. Most construction job sites and workshops maintain a dedicated waste oil drum that is collected by professional disposal services.
When disposing of oil, keep it in a leak-proof, labeled container. If working on a residential project, locate the nearest municipal hazardous waste facility to ensure compliance with local environmental regulations.
Bottom line: Responsible disposal is a mandatory part of professional conduct. Protect the environment and stay compliant by treating used oil as the hazardous material it is.
Maintaining the integrity of your vacuum pump with the right oil is a hallmark of a professional. By consistently using the correct lubricant and changing it religiously, you ensure that every evacuation is thorough and every system is ready for a long, reliable service life.